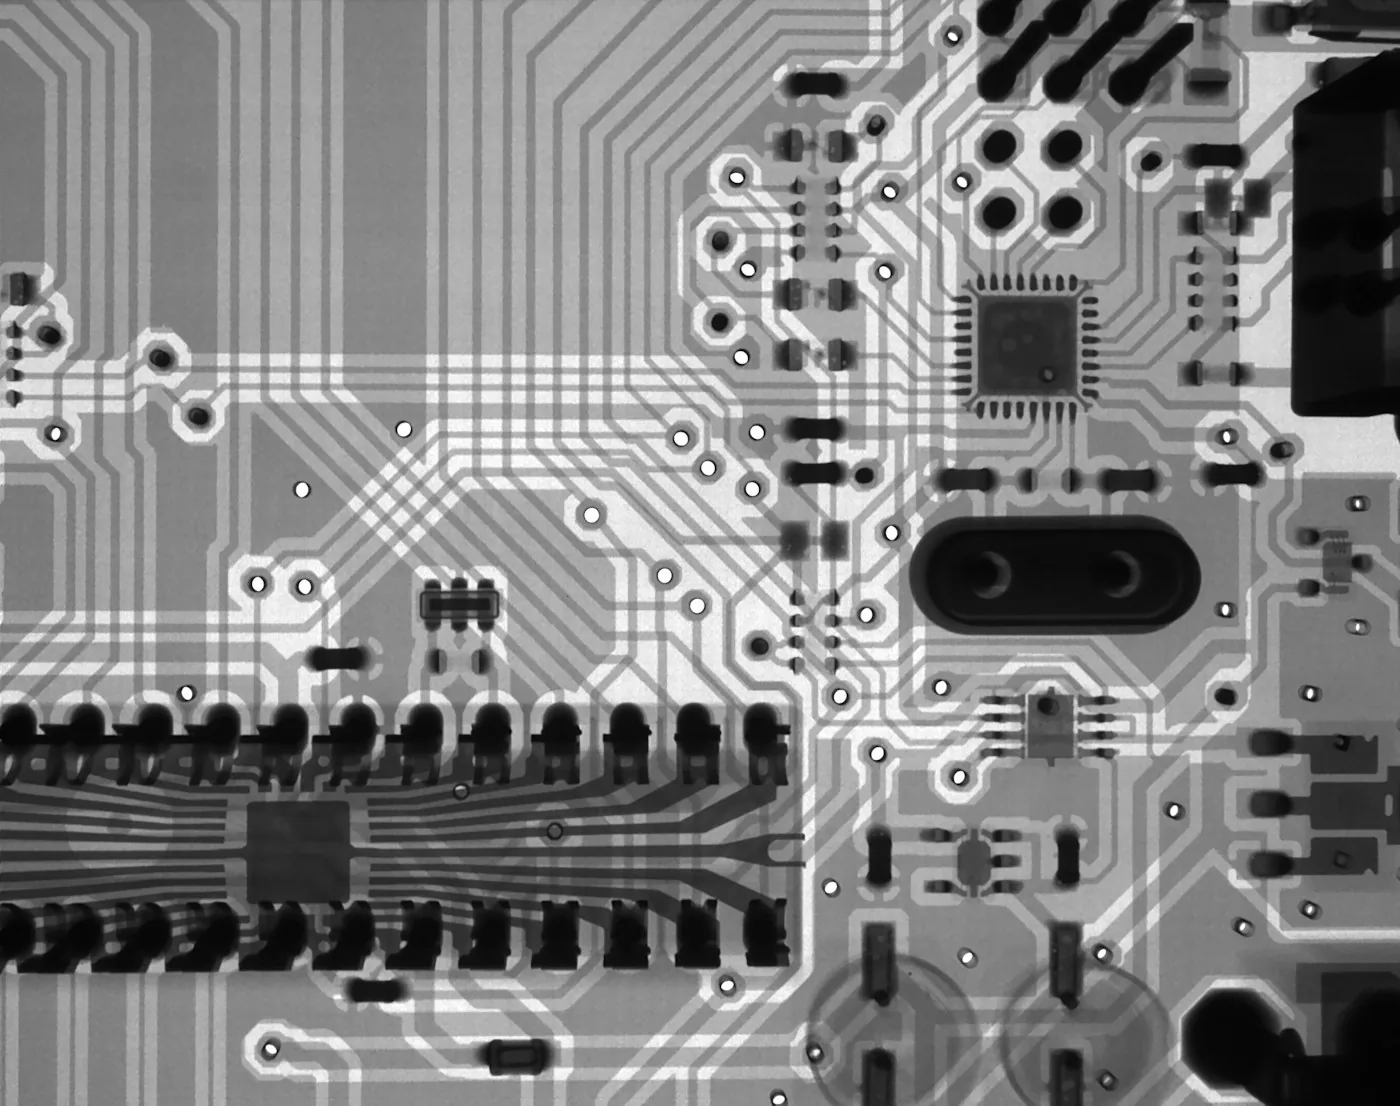
Assessing void indications beneath BGAs and thermal pads requires the package geometry, electrical or thermal function, and inspection view to be considered together. A process review can connect solder-paste print data, a profile measured for the product assembly, and X-ray images, while keeping each method's limits clear. BGA review depends on agreed inspection scope, measurement basis, acceptance criteria, and disposition for the actual assembly. SPI describes paste deposits before placement; X-ray helps examine hidden joints after soldering. Neither result alone proves circuit function or long-term reliability.
Review stencil apertures for the design
Thermal-pad windowing, aperture dimensions, stencil thickness, paste, board support, and cleaning can affect the deposit. Review these factors with pad and package geometry, nearby components, board constraints, supplier process evidence, and applicable design rules. Treat settings as design- and process-specific; verify proposed changes on a representative build before release.
Measure a representative reflow profile
Board thickness, copper distribution, component mass, paste specification, and adjacent parts influence temperature during reflow. Agree how the profile will be measured on a representative assembly, where thermocouples will be placed, which component limits apply, and how deviations are reviewed. A coupon may help monitor a process but does not automatically represent every production board.
Use SPI and X-ray as complementary checks
- Use SPI results to review paste deposits at agreed BGA or thermal-pad locations before placement.
- Use X-ray views agreed for the package and board to assess hidden-joint features and void indications after reflow.
- Compare records by board or lot and investigate patterns with the supplier. Correlation can guide a process review, but does not alone establish root cause.
Set project-specific acceptance criteria
Do not apply one void percentage to every design. In the RFQ, identify the product or customer requirement, any invoked standard and revision, inspection coverage, image view and measurement basis, decision owner, retained evidence, and disposition path. IPC-A-610 is an assembly-acceptance reference; IPC-7095 provides BGA design and assembly guidance. Agree how the specified documents apply to the order, including class or product-specific exceptions. For thermal pads, consider the stated thermal or electrical function as well as the measurement method. Confirm revisions with IPC or the customer before naming them in the purchase requirements.
Discuss process evidence during NPI
For NPI, share the operating conditions, electrical and thermal requirements, package data, and board files. Ask the supplier to confirm which SPI, X-ray, profile-measurement, and review activities are feasible for the build. See the capability and sourcing questions and include the requested scope in the RFQ.